Call:
 Send Inquiry

 Send Inquiry
Bucket Elevator Conveyor
MOQ : 1 Unit
Bucket Elevator Conveyor Specification
- Belt Type
- Modular plastic or rubber belt
- Thickness
- 5-8 mm (belt/bucket)
- Features
- Low maintenance, high efficiency, gentle handling of material
- Surface Finish
- Polished/smooth finish
- Power Source
- Electric
- Material
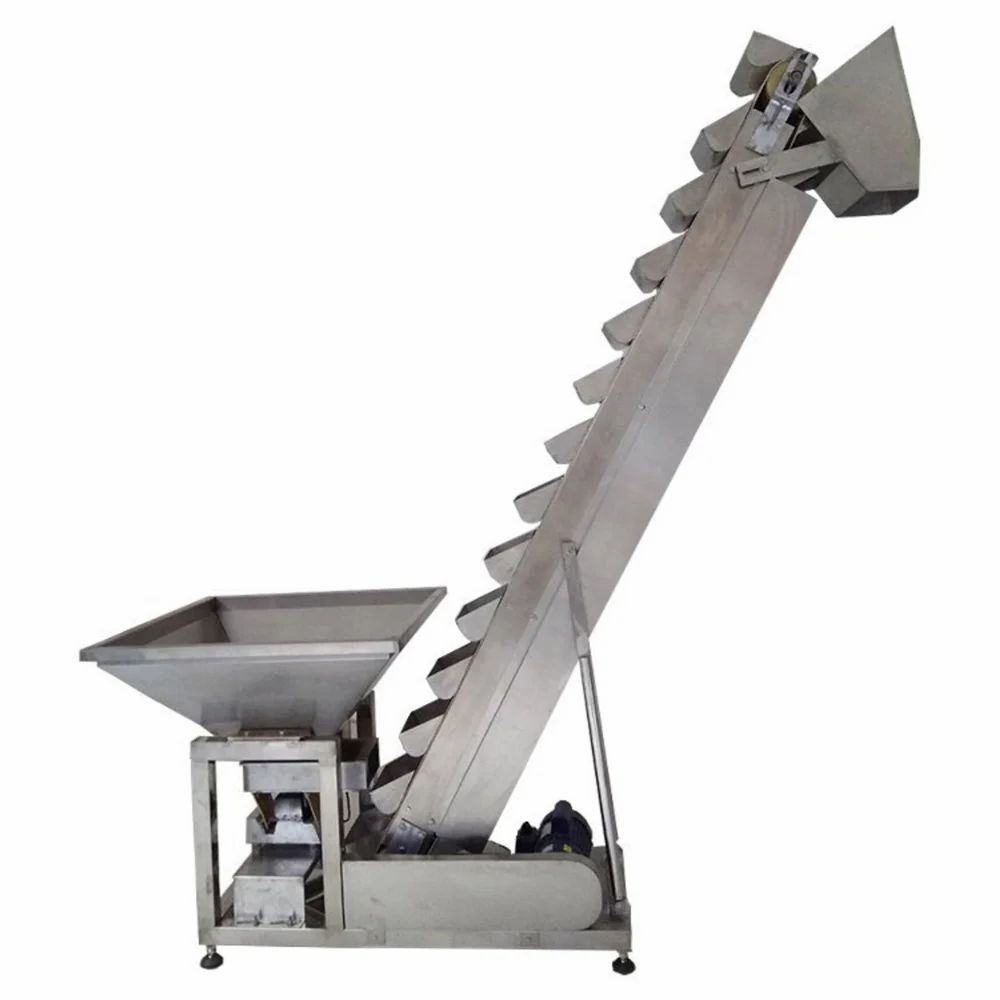
- Food grade plastic buckets, stainless steel construction
- Type
- Bucket Elevator Conveyor
- Structure
- Inclined or vertical as per design
- Belt Conveyor
- Yes, with bucket attachments
- Roller Conveyor
- No
- Vertical Conveyor
- Yes
- Pneumatic Conveyor
- No
- Resistant Feature
- Corrosion and wear resistant
- Load Capacity
- Customizable as per requirement
- Voltage
- 220-440V
- Power
- 1-5 HP (optional)
- Speed
- Variable, typically 1-2 m/s
- Usage & Applications
- Grain handling, packaging lines, food industry, bulk material transport
- Safety Features
- Emergency stop, overload protection
- Drive Type
- Geared motor drive
- Bucket Volume
- 1 to 10 liters per bucket (customizable)
- Discharge Height
- Up to 20 meters
- Finish Options
- Powder coated, galvanized, or SS finish available
- Colour
- Blue (standard), customizable
- Installation Type
- Floor mounted
- Noise Level
- < 70 dB
- Control System
- Manual or automated (PLC compatible)
- Design Standards
- Conforms to BIS/ISO/CE standards
- Customization
- Bucket material, belt length, and speed adjustable
- Maintenance
- Easy bucket and belt replacement
- Operating Temperature
- -10C to 60C
Bucket Elevator Conveyor Trade Information
- Minimum Order Quantity
- 1 Unit
- Payment Terms
- Cash in Advance (CID)
- Supply Ability
- 10 Units Per Month
- Delivery Time
- 5-7 Days
- Main Domestic Market
- All India
About Bucket Elevator Conveyor
Buy online the top-tier Bucket Elevator Conveyor, engineered for pristine, high-efficiency performance across a wide temperature range (-10C to 60C). Purpose-built for grain handling, packaging lines, and the food industry, this redoubtable solution features food-grade plastic buckets, stainless steel construction, and customizable capacities. Explore superior safety features including emergency stop and overload protection, plus easy maintenance with quick bucket and belt replacement. Available with polished, powder coated, or SS finish, this conveyor ensures a polished appearance, robust corrosion resistance, and smooth, gentle handling every time. Conforms to BIS/ISO/CE standards for reliability.
Polished Performance and Versatile Application
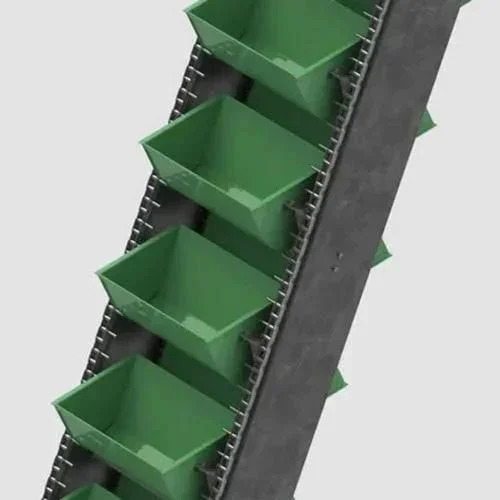
The Bucket Elevator Conveyor boasts key features like customizable bucket volume, adjustable belt speed, and a corrosion-resistant stainless steel frame. Designed for installation in floor-mounted setups, it excels in bulk material transport, gentle grain handling, and food packaging lines. Used as a vertical conveying system, it ensures pristine and efficient movement of products, striking a balance between durability and polished aesthetics. Its modular belt makes it adaptable to diverse material-handling environments.
Export Logistics and Impressive Supply Capacity
Our Bucket Elevator Conveyor enjoys strong demand in international markets due to reliable supply ability. Carefully packaged, each unit is handed over for shipment via major Indian FOB ports, optimizing logistics for timely global dispatch. Our professional export valuation meets international standards, ensuring cost transparency. Whether for industrial importers or automated packaging integrators, our streamlined logistics and communication guarantee secure, on-time deliveries worldwide.
Polished Performance and Versatile Application
The Bucket Elevator Conveyor boasts key features like customizable bucket volume, adjustable belt speed, and a corrosion-resistant stainless steel frame. Designed for installation in floor-mounted setups, it excels in bulk material transport, gentle grain handling, and food packaging lines. Used as a vertical conveying system, it ensures pristine and efficient movement of products, striking a balance between durability and polished aesthetics. Its modular belt makes it adaptable to diverse material-handling environments.
Export Logistics and Impressive Supply Capacity
Our Bucket Elevator Conveyor enjoys strong demand in international markets due to reliable supply ability. Carefully packaged, each unit is handed over for shipment via major Indian FOB ports, optimizing logistics for timely global dispatch. Our professional export valuation meets international standards, ensuring cost transparency. Whether for industrial importers or automated packaging integrators, our streamlined logistics and communication guarantee secure, on-time deliveries worldwide.
FAQ's of Bucket Elevator Conveyor:
Q: How does the bucket elevator conveyor operate for bulk material handling?
A: The conveyor utilizes robust buckets attached to a modular belt that move vertically or at an incline, efficiently transporting bulk materials such as grains or processed foods to designated discharge points up to 20 meters high.Q: What safety features are included in the bucket elevator conveyor?
A: The model is equipped with emergency stop and overload protection to ensure operator safety and protect machinery during routine use and unexpected events.Q: When should I opt for customization in bucket volume, speed, or material?
A: Customization is recommended when processing material with unique size, weight, or handling characteristics, or when adapting to pre-existing facility layouts or throughput needs for optimum performance.Q: Where can the conveyor be installed within a facility?
A: It is designed for floor-mounted installation and can be configured in vertical or inclined orientations to match available space and process flow within grain storage, food packaging, or industrial material handling sectors.Q: What is the process for regular maintenance of this conveyor?
A: Routine maintenance includes inspecting belt tension, checking bucket attachment points, and replacing buckets or belts as necessary-tasks made easy by user-centric design for minimal downtime.Q: What are the main benefits of choosing this conveyor for industrial applications?
A: Key advantages include low operating noise, modular customization, gentle and efficient handling of sensitive materials, corrosion and wear resistance, and compliance with international design standards.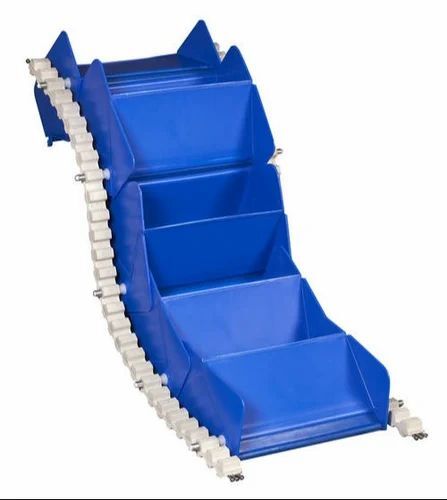
More Products in Industial Conveyors Category
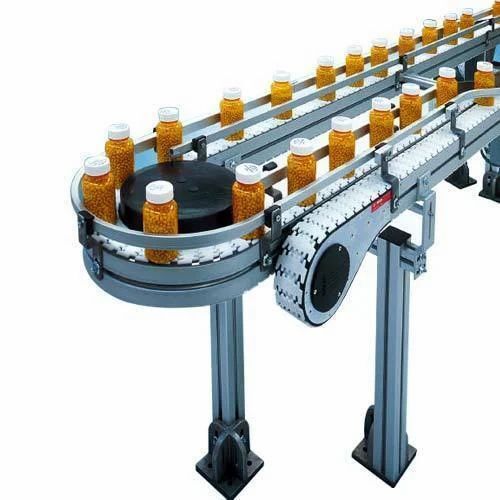
Bottle Transfer Conveyor
Minimum Order Quantity : 1 Unit
Speed : 5 to 60 m/min adjustable
Structure : Other, Modular Frame with Aluminum/Steel Legs
Voltage : 220 V / 380 V
Pneumatic Conveyor : Other, No
Roller Conveyor : Other, No
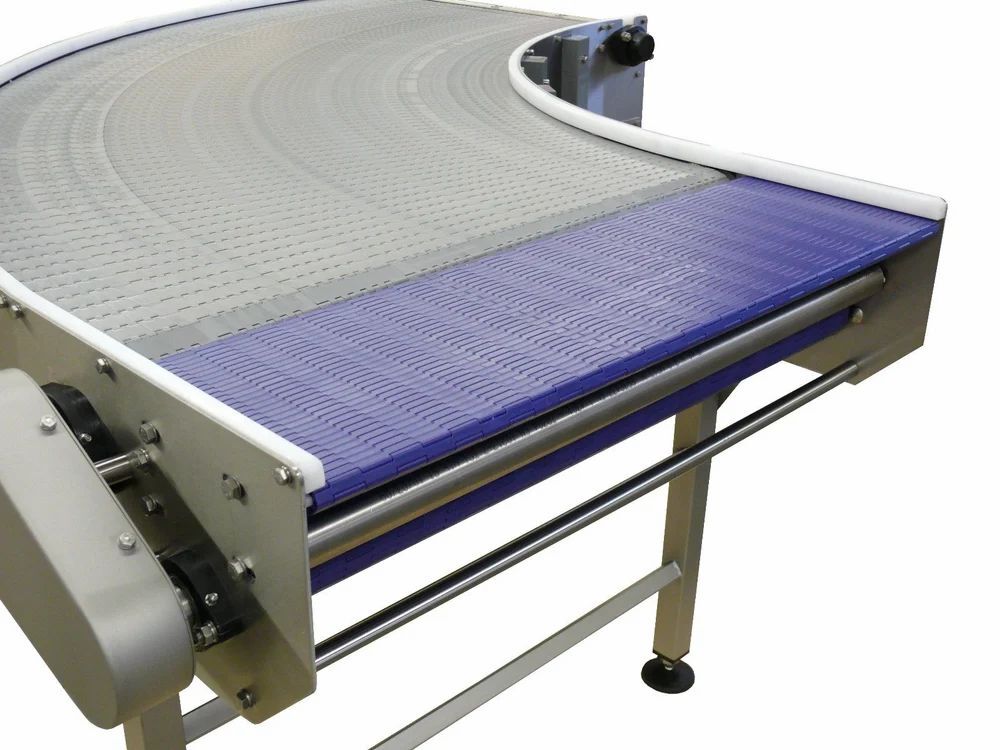
90° Radius Conveyor
Minimum Order Quantity : 1 Unit
Speed : 10 30 m/min (variable)
Structure : Other, Mild Steel or Stainless Steel Frame
Voltage : 220V / 380V (as per requirement)
Pneumatic Conveyor : Other, No
Roller Conveyor : Other, No (but option available upon request)
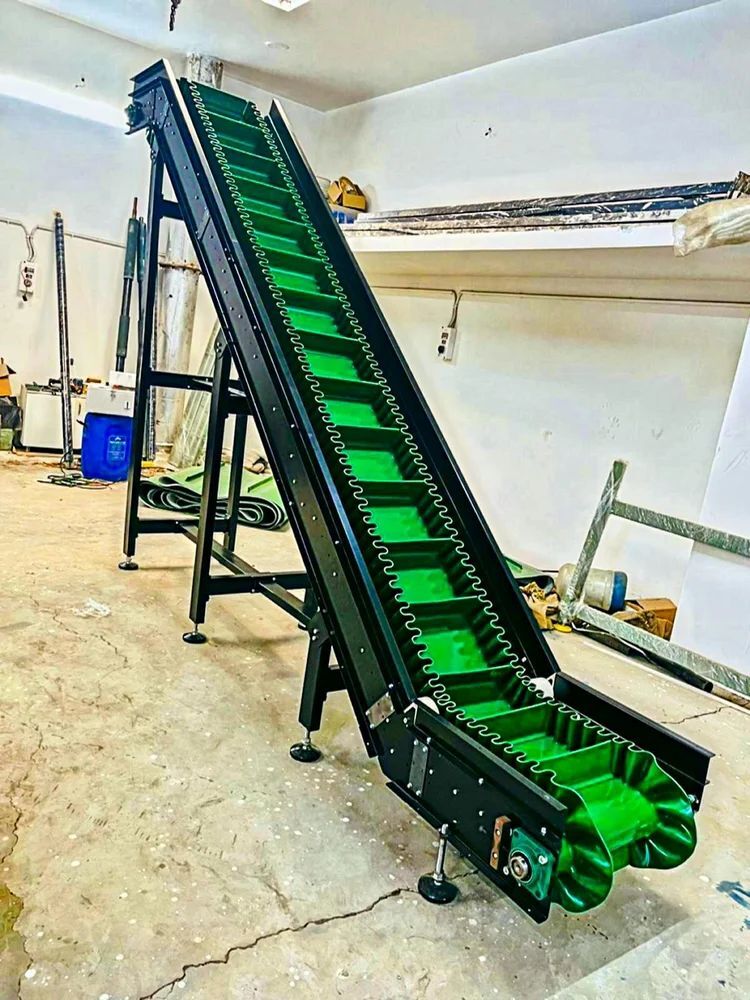
Cleated Belt Conveyor
Minimum Order Quantity : 1 Unit
Speed : Adjustable, typically 1060 m/min
Structure : Other, Mild steel frame with powder coating
Voltage : 220415 V AC (as per requirement)
Pneumatic Conveyor : Other, No
Roller Conveyor : Other, No
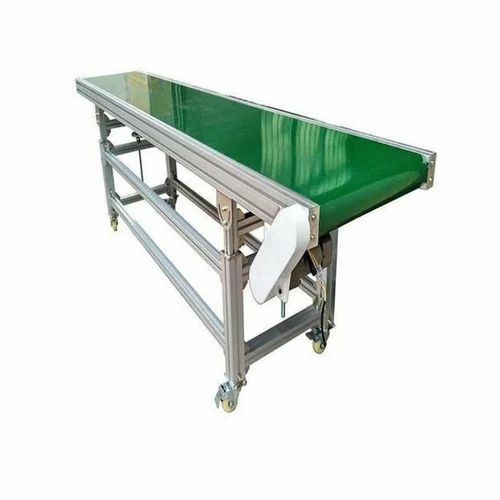
PVC Flat Belt Conveyor
Minimum Order Quantity : 1 Unit
Speed : Variable, typically 1030 m/min
Structure : Other, Stainless Steel Frame
Voltage : 220240V AC
Pneumatic Conveyor : Other, No
Roller Conveyor : Other, No

Contact Details
GST : 29GDBPK3496J1ZZ
- B No 53, Near Sri Ambamaheshwari Temple, 7th Main Road,Bengaluru - 560079, Karnataka, India
 Send Inquiry

Developed and Managed by Infocom Network Private Limited.


