Call:
 Send Inquiry

 Send Inquiry
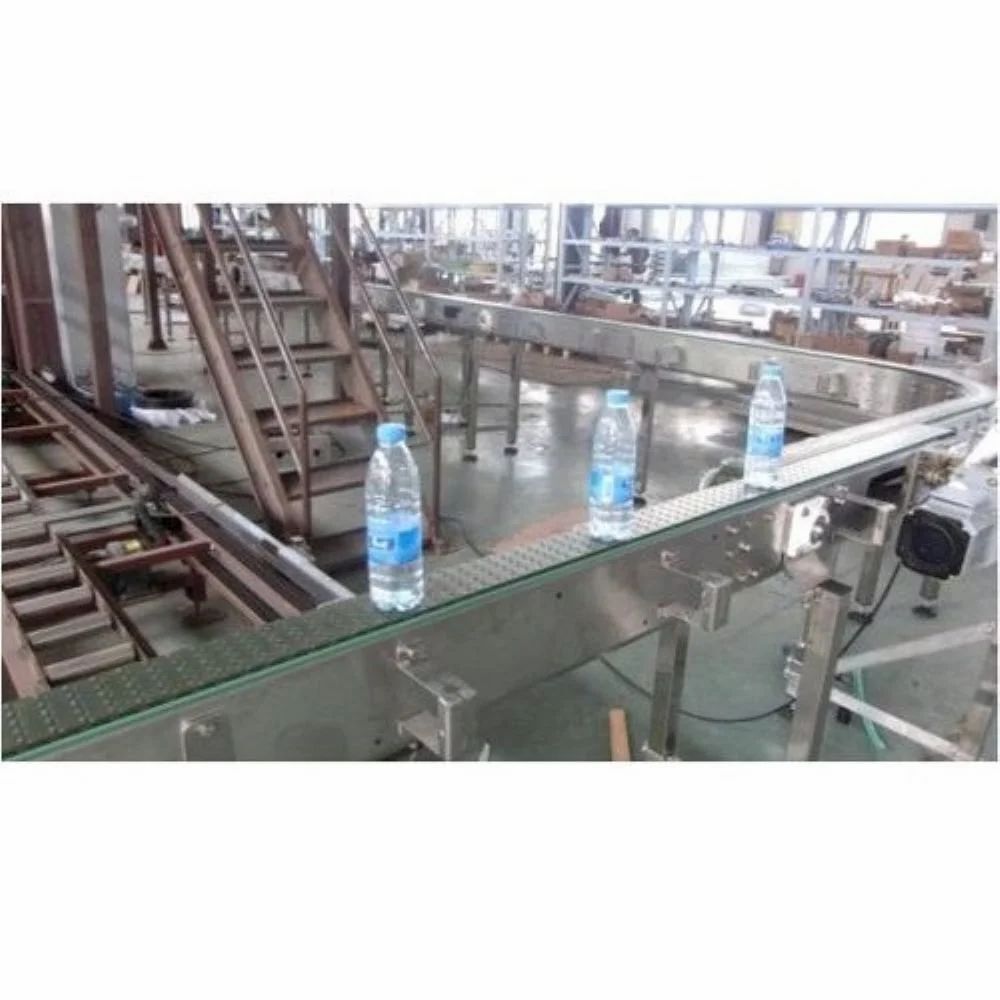
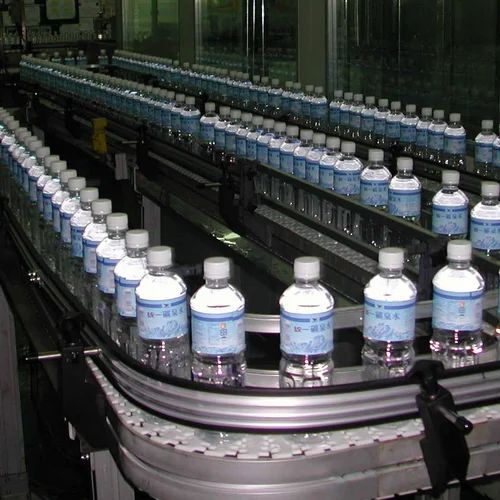
Bottle Transfer Conveyor
MOQ : 1 Unit
Bottle Transfer Conveyor Specification
- Power Source
- Electric
- Features
- Durable, Low Maintenance, High Speed, Smooth Operation
- Surface Finish
- Polished or Powder Coated
- Thickness
- 3 mm (belt)
- Belt Type
- Modular Plastic Chain Belt
- Material
- Stainless Steel & Aluminium
- Type
- Bottle Transfer Conveyor
- Structure
- Modular Frame with Aluminum/Steel Legs
- Belt Conveyor
- Yes
- Roller Conveyor
- No
- Vertical Conveyor
- No
- Pneumatic Conveyor
- No
- Resistant Feature
- Corrosion Resistant
- Load Capacity
- Up to 50 kg per meter
- Voltage
- 220 V / 380 V
- Power
- 0.75 - 2.2 kW
- Speed
- 5 to 60 m/min adjustable
- Usage & Applications
- Bottling, Packaging, Food & Beverage, Pharmaceutical
- Control System
- PLC / Manual Switch
- Frame Material
- Anodized Aluminium / SS 304
- Maintenance
- Minimal, Tool-free Chain Dismantling
- Noise Level
- Low Noise Operation
- Height Adjustment
- Adjustable leg height
- Conveyor Length
- 3 to 30 meters (customizable)
- Width
- 80 mm to 300 mm
- Direction of Movement
- Unidirectional or Reversible
- Drive Type
- Motorized
- Chain Material
- Food Grade Plastic
- Installation
- Easy to Assemble & Install
Bottle Transfer Conveyor Trade Information
- Minimum Order Quantity
- 1 Unit
- Payment Terms
- Cash in Advance (CID)
- Supply Ability
- 10 Units Per Month
- Delivery Time
- 5-7 Days
- Main Domestic Market
- All India
About Bottle Transfer Conveyor
Unlock astounding efficiency with our Bottle Transfer Conveyor, engineered for brilliant performance in bottling, packaging, food & beverage, and pharmaceutical industries. Featuring a modular, corrosion-resistant frame in anodized aluminium or SS 304, the conveyor is customizable from 3 up to 30 meters. Enjoy low-noise operation, excellent durability, and minimal maintenance. Its adjustable height, food grade plastic chain, and tool-free dismantling make assembly and use remarkably easy. Capable of handling up to 50 kg/meter and available with PLC/manual controls, this exclusive system ensures smooth, high-speed transfer. Try Now for an excellent bottling solution!
Astounding Advantages & Diverse Applications
This Bottle Transfer Conveyor excels in multiple sectors, seamlessly integrating into bottling lines, food processing, pharmaceutical production, and comprehensive packaging solutions. Its durable, polished or powder-coated surface supports reliable operation on a range of surfaces, while the corrosion-resistant materials ensure longevity. Enjoy the advantage of quiet and swift transportation of bottles, enabling consistent and smooth workflow across varied production environments. The adjustable features and modular structure make it easy to fit into both new and existing setups for optimum results.
Secure Shipping & Reliable Packaging Information
Your Bottle Transfer Conveyor reaches you with secure packaging that ensures product integrity during transit. Our stock is ready for quick dispatch via express shipping from major Indian FOB ports. Each unit is shipped with necessary certifications for quality and safety, offering assurance and value. Whether you need one conveyor or a fleet, our streamlined logistics and ready stock mean your production upgrade arrives on time and in excellent condition, prepared for immediate implementation.
Astounding Advantages & Diverse Applications
This Bottle Transfer Conveyor excels in multiple sectors, seamlessly integrating into bottling lines, food processing, pharmaceutical production, and comprehensive packaging solutions. Its durable, polished or powder-coated surface supports reliable operation on a range of surfaces, while the corrosion-resistant materials ensure longevity. Enjoy the advantage of quiet and swift transportation of bottles, enabling consistent and smooth workflow across varied production environments. The adjustable features and modular structure make it easy to fit into both new and existing setups for optimum results.
Secure Shipping & Reliable Packaging Information
Your Bottle Transfer Conveyor reaches you with secure packaging that ensures product integrity during transit. Our stock is ready for quick dispatch via express shipping from major Indian FOB ports. Each unit is shipped with necessary certifications for quality and safety, offering assurance and value. Whether you need one conveyor or a fleet, our streamlined logistics and ready stock mean your production upgrade arrives on time and in excellent condition, prepared for immediate implementation.
FAQ's of Bottle Transfer Conveyor:
Q: How is the Bottle Transfer Conveyor installed?
A: Installation is quick and hassle-free, thanks to its modular frame and easy-to-assemble components. Adjustable leg height and tool-free chain dismantling further simplify the setup process.Q: What makes this conveyor an excellent choice for bottling and packaging industries?
A: Its corrosion-resistant materials, durable structure, and high-load capacity, combined with low maintenance and smooth operation, make it an ideal solution for demanding bottling and packaging lines.Q: When should I consider upgrading to a motorized Bottle Transfer Conveyor?
A: You should consider upgrading when you need higher transfer speeds, improved workflow efficiency, or when expanding production capacity in food, beverage, or pharmaceutical facilities.Q: Where can the Bottle Transfer Conveyor be applied?
A: It is highly suitable for applications in bottling plants, food processing units, pharmaceutical manufacturing, and general packaging industries.Q: What is the process for adjusting the speed and direction of operation?
A: Speed can be adjusted between 5 to 60 meters per minute using the control system (PLC or manual switch). The direction can be set as either unidirectional or reversible, depending on your workflow requirements.Q: What benefits does the modular design offer?
A: The modular frame allows customization of length and layout, easy installation, effortless maintenance, and adaptability to various production setups.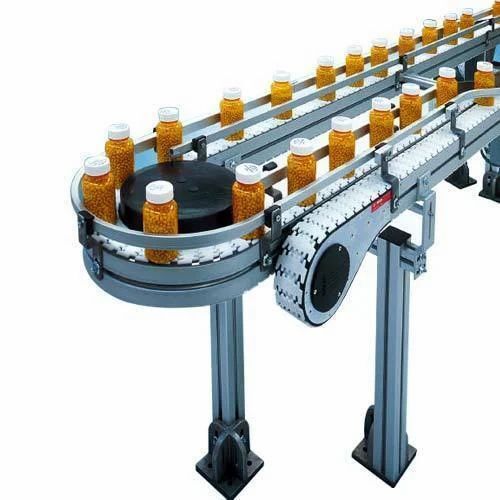
More Products in Industial Conveyors Category
180° Radius Conveyor
Minimum Order Quantity : 1 Unit
Thickness : Belt thickness 25 mm
Belt Conveyor : Other, Yes
Speed : 0.21.5 m/s (variable)
Power : 0.52.5 kW (dependent on length and load)
Resistant Feature : Other, Corrosionresistant, Wearresistant
Metal Chip Conveyor
Minimum Order Quantity : 1 Unit
Thickness : 3 mm 8 mm sheets used
Belt Conveyor : Other, Yes
Speed : 2 to 20 m/min (variable)
Power : 0.5 3 HP
Resistant Feature : Other, Corrosion and abrasion resistant
Vertical Continous Conveyor
Minimum Order Quantity : 1 Unit
Thickness : Frame: 510 mm
Belt Conveyor : Other, Optional Unit Integration
Speed : 0.1 1 m/s (adjustable)
Power : 13 HP, variable as per model
Resistant Feature : Other, Corrosion Resistant, Wear Resistant
Knife Edge Belt Conveyor
Minimum Order Quantity : 1 Unit
Thickness : 1.5 3 mm (Belt)
Belt Conveyor : Other, Yes
Speed : 0.1 1 m/s (variable)
Power : 0.5 2 HP
Resistant Feature : Other, Corrosion Resistant, Rustproof

Contact Details
GST : 29GDBPK3496J1ZZ
- B No 53, Near Sri Ambamaheshwari Temple, 7th Main Road,Bengaluru - 560079, Karnataka, India
 Send Inquiry

Developed and Managed by Infocom Network Private Limited.


