Call:
 Send Inquiry

 Send Inquiry
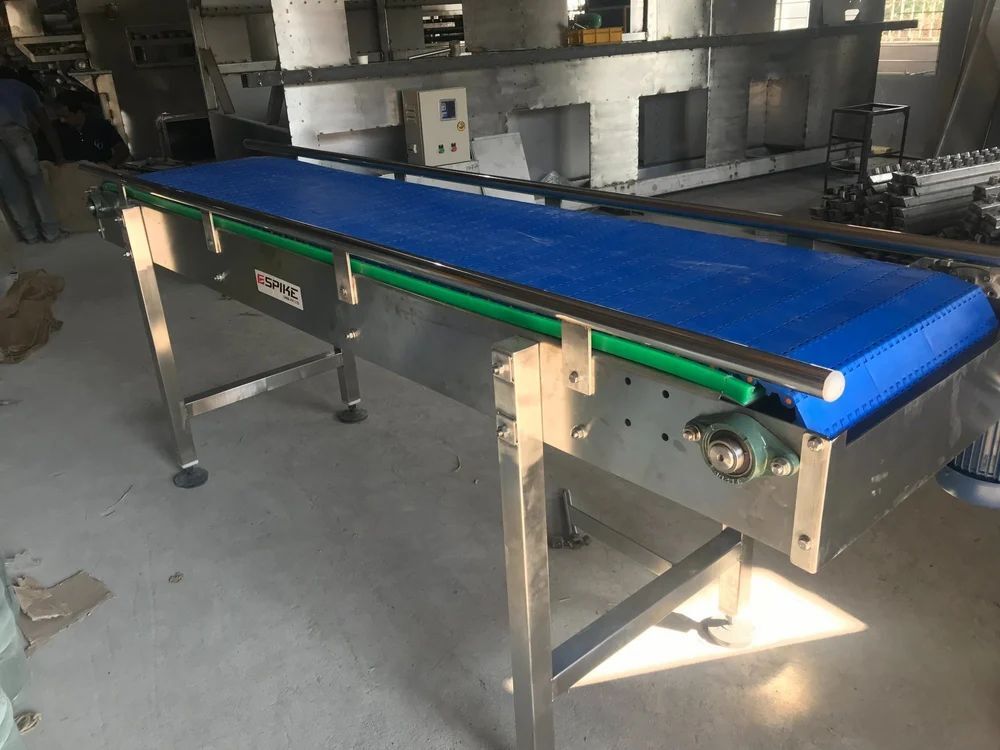
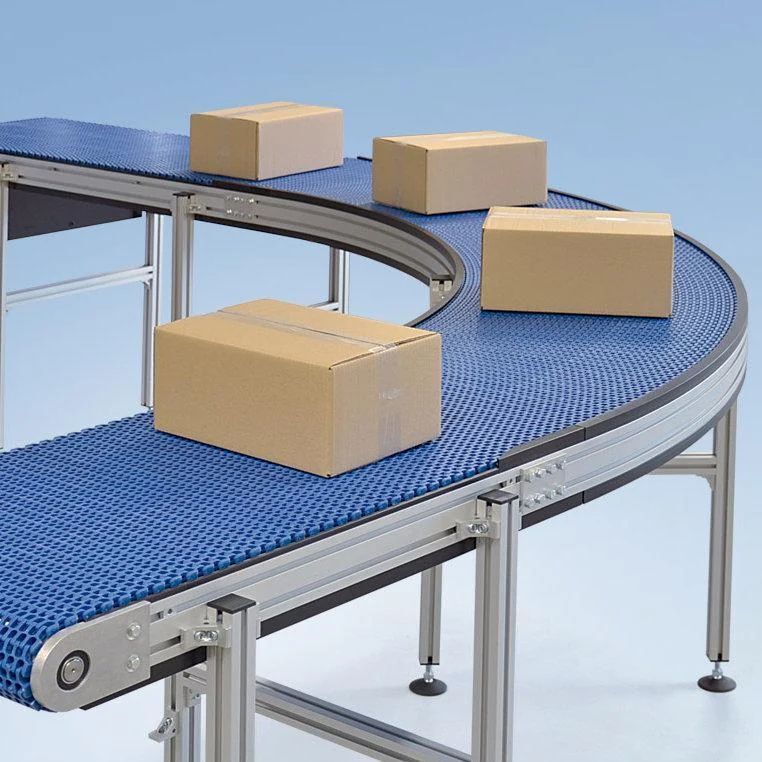
Modular Belt Conveyor
MOQ : 1 Unit
Modular Belt Conveyor Specification
- Features
- Easy to clean, modular design, high reliability, low maintenance, customizable length & width
- Power Source
- Electric
- Surface Finish
- Polished / Food-Grade (based on demand)
- Belt Type
- Modular plastic belt (flush grid or flat top depending on item)
- Thickness
- Belt thickness 10-20 mm (approx, varies by model)
- Material
- Polypropylene/Polyethylene modular belt, Stainless Steel body
- Type
- Modular Belt Conveyor
- Structure
- Stainless Steel frame (SS304/SS316)
- Belt Conveyor
- Yes
- Roller Conveyor
- No
- Vertical Conveyor
- Available (Design dependent on requirement)
- Resistant Feature
- Corrosion & wear resistant, suitable for food-grade applications
- Load Capacity
- Customizable as per application requirements
- Voltage
- 220-415 V, 3 Phase (customizable as requested)
- Power
- 0.75 kW - 2.2 kW (based on conveyor size and application)
- Speed
- Variable (adjustable as per operational need)
- Usage & Applications
- Food processing, packaging lines, pharmaceutical, logistics, general material handling
- Height Adjustment
- Manual or automatic, as requested
- Noise Level
- Low (Below 70 dB during standard operation)
- Cleaning Method
- Quick-release belt, open structure for easy washdown
- Chain Type
- Acetal or low-friction chain options available
- Belt Width
- Varies from 200 mm to 1500 mm (customized as per process)
- Incline Angle
- Adjustable up to 60 based on model
- Max Operating Temperature
- Up to 80C (belt and components)
- Safety Features
- Emergency stop switches, side guiderails
- Drive Type
- Direct shaft or End-drive motor mounted
Modular Belt Conveyor Trade Information
- Minimum Order Quantity
- 1 Unit
- Payment Terms
- Cash in Advance (CID)
- Supply Ability
- 10 Units Per Month
- Delivery Time
- 5-7 Days
- Main Domestic Market
- All India
About Modular Belt Conveyor
Experience unmatchable efficiency with our Featured Modular Belt Conveyor, tailored for food processing, packaging lines, pharmaceuticals, logistics, and general material handling. Boasting a robust stainless steel frame and corrosion-resistant, food-grade modular belts, this noteworthy conveyor offers perfect cleaning convenience with a quick-release system. Enjoy operation at below 70 dB, customizable incline angles and speed, and safety features like emergency stop switches. Enjoy the best price on sale-ideal for demanding applications with customizable load capacity, belt width, and drive types. Reliable, easy to maintain, and built to last, our modular belt conveyor stands out as an industry leader in India.
Versatile Industrial Conveyor Applications
Our Modular Belt Conveyor is perfectly suited for application media such as processed foods, pharmaceuticals, and packaging materials. Its use type includes material conveying on inclined surfaces, sorting, and assembly. Designed to be adaptable, it's suitable for use in food processing plants, pharmaceutical cleanrooms, packaging lines, and logistics warehouses. The customizable structure ensures you get the right conveyor for your operational environment, delivering high performance with enhanced reliability across various demanding industry sectors.
Payment Terms, Domestic Market & FOB Port
We accept flexible payment terms to ensure a smooth packaging and shipping process. The main domestic market for our Modular Belt Conveyor is India, meeting diverse industrial needs with tailored solutions. FOB Port options are available for easy and cost-effective export. The outlay for each unit reflects its premium features and dependable quality, making it a wise expenditure for businesses looking to optimize their productivity and streamline operations within budget.
Versatile Industrial Conveyor Applications
Our Modular Belt Conveyor is perfectly suited for application media such as processed foods, pharmaceuticals, and packaging materials. Its use type includes material conveying on inclined surfaces, sorting, and assembly. Designed to be adaptable, it's suitable for use in food processing plants, pharmaceutical cleanrooms, packaging lines, and logistics warehouses. The customizable structure ensures you get the right conveyor for your operational environment, delivering high performance with enhanced reliability across various demanding industry sectors.
Payment Terms, Domestic Market & FOB Port
We accept flexible payment terms to ensure a smooth packaging and shipping process. The main domestic market for our Modular Belt Conveyor is India, meeting diverse industrial needs with tailored solutions. FOB Port options are available for easy and cost-effective export. The outlay for each unit reflects its premium features and dependable quality, making it a wise expenditure for businesses looking to optimize their productivity and streamline operations within budget.
FAQ's of Modular Belt Conveyor:
Q: How is the Modular Belt Conveyor cleaned and maintained?
A: The conveyor features a quick-release belt and open structure, facilitating easy washdown and minimal downtime. Its design enables fast and thorough cleaning, which is perfect for food-grade and pharmaceutical applications.Q: What industries benefit from using this Modular Belt Conveyor?
A: It is ideal for industries like food processing, packaging, pharmaceuticals, logistics, and general material handling, thanks to its robust stainless steel construction and modular, customizable design.Q: Where can this conveyor be installed?
A: This conveyor can be installed in various settings such as manufacturing floors, packaging facilities, warehouses, cleanrooms, and logistics centers, offering flexibility due to its adjustable dimensions and features.Q: What are the safety features included in the conveyor?
A: Safety is prioritized with features like emergency stop switches and side guiderails, ensuring secure operation and offering peace of mind during both standard and intensive industrial use.Q: What is the benefit of the customizable incline angle and belt width?
A: Customizable incline angles (up to 60) and variable belt width (200-1500mm) allow seamless adaptation to your process requirements, ensuring optimal material flow and space utilization.Q: How does the modular design affect installation and usage?
A: The modular design allows for quick assembly, flexibility in length or configuration, easy upgrades, and efficient repairs-leading to reduced downtime and enhanced reliability.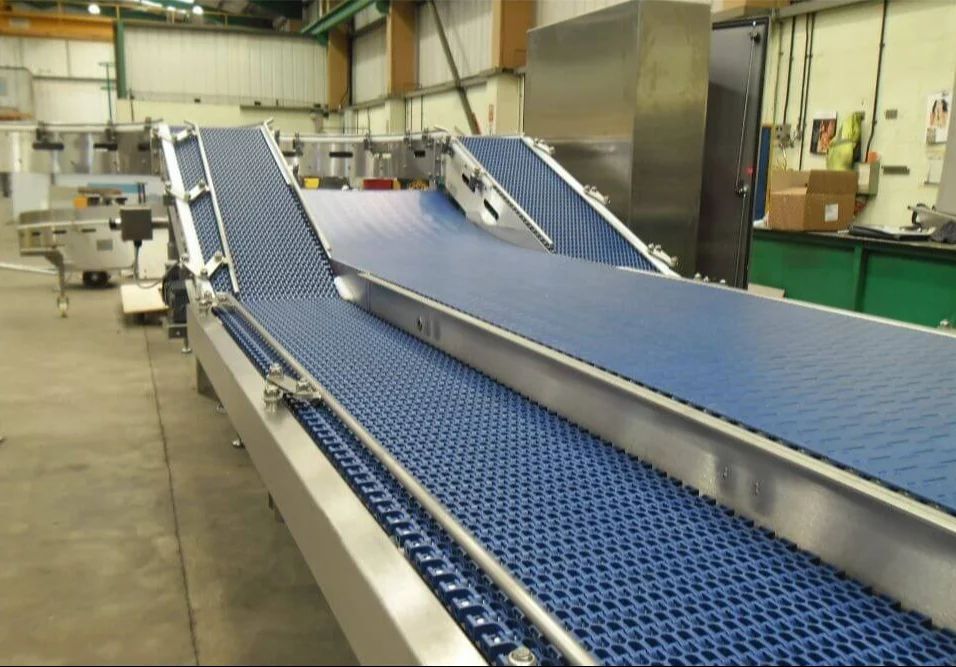
More Products in Industial Conveyors Category
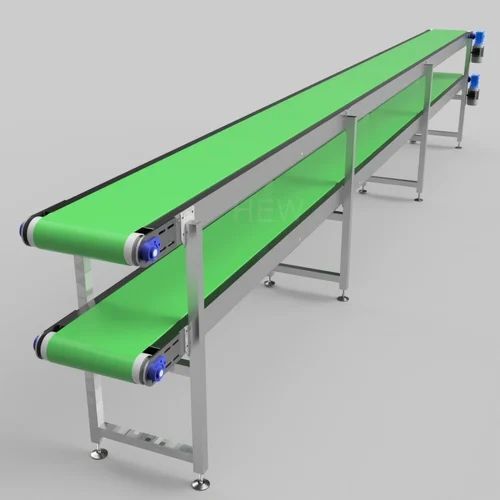
Double Decker Conveyor
Minimum Order Quantity : 1 Unit
Pneumatic Conveyor : Other, No
Material : Mild steel frame with powder coating or stainless steel; PVC/Rubber belt
Type : Other, Double Decker Conveyor
Thickness : Frame: 23 mm; Belt: 3 mm average
Usage & Applications : Assembly lines, warehouses, packaging, electronics, manufacturing
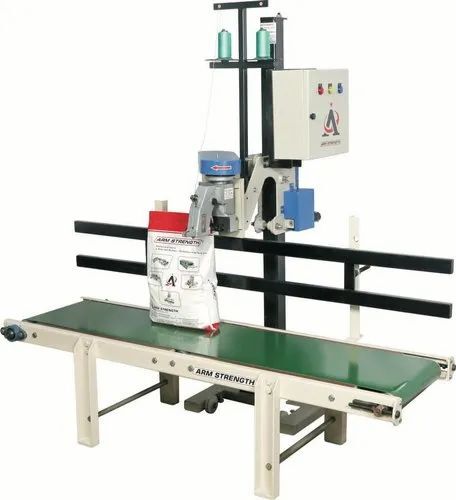
Automatic Bag Closing Conveyor
Minimum Order Quantity : 1 Unit
Pneumatic Conveyor : Other, No
Material : Mild Steel, Powder Coated/SS Option
Type : Other, Automatic Bag Closing Conveyor
Thickness : Belt Thickness 3 mm
Usage & Applications : Suitable for bag closing in sectors like food processing, grains, fertilizer, chemicals, cement, and seeds
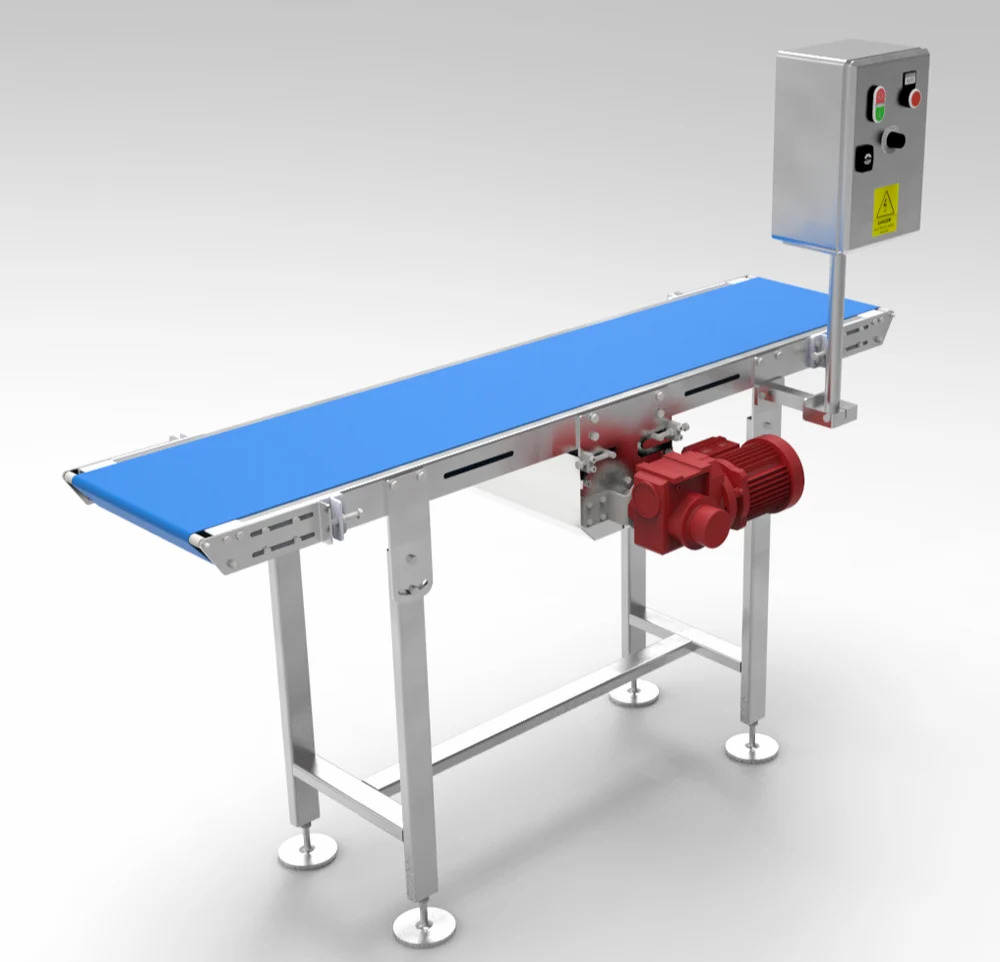
Knife Edge Belt Conveyor
Minimum Order Quantity : 1 Unit
Pneumatic Conveyor : Other, No
Material : Stainless Steel, PU Belt
Type : Other, Knife Edge Belt Conveyor
Thickness : 1.5 3 mm (Belt)
Usage & Applications : Food Industry, Pharmaceuticals, Packaging, Assembly Lines
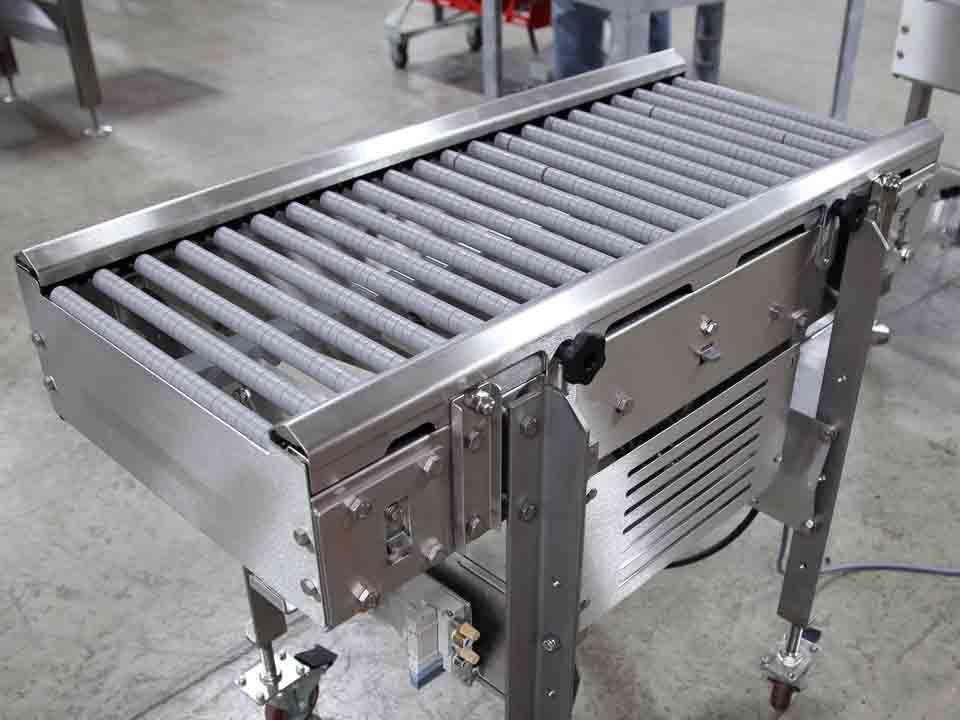
SS Roller Conveyor
Minimum Order Quantity : 1 Unit
Pneumatic Conveyor : Other, No
Material : Stainless Steel (SS 304/316)
Type : Roller Conveyor
Thickness : 23 mm (frame and roller wall thickness)
Usage & Applications : Material handling in food, pharmaceutical, packaging, cosmetic, and general industrial sectors

Contact Details
GST : 29GDBPK3496J1ZZ
- B No 53, Near Sri Ambamaheshwari Temple, 7th Main Road,Bengaluru - 560079, Karnataka, India
 Send Inquiry

Developed and Managed by Infocom Network Private Limited.


